


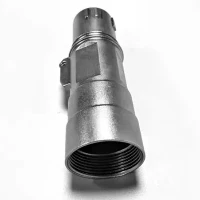
Stainless Steel High Voltage Parts
Name: Stainless Steel high voltage parts
Material: stainless steel
Application process: customized processing + precision casting / forging / profile + surface treatment
Main use: used in building sanitary industry pipeline industry
Production Detailes:
Name:Stainless Steel high voltage parts
Material: stainless steel
Application process: customized processing + precision casting / forging / profile + surface treatment
Main use: used in building sanitary industry pipeline industry
| Casting | Description |
|---|---|
|
Name |
Stainless Steel valve casting parts |
|
Material |
Stainless steel |
|
Process |
customized processing + precision casting+ surface treatment |
|
Processing equipment |
CNC lathe with inclined bed |
|
Surface Treatment |
Electropolishing+pickling passivation of nickel+chromium plating |
|
Casting surface roughness |
Ra0.8-1.6 |
|
Heat treatment |
solid solution treatment (1050 ℃ for more than 2 h) |
|
Measuring tools |
CMM, Micrometer, Inner diameter Gauge, Height Gauge, Flow Detector |
|
Inspection method |
Three inspection: First Inspection, Patrol Inspection and Final Inspection (Flow and Pressure Measurement) |
|
Reports available |
Glass clip Material Cert., Product Dimensional Inspection Report. |
Product Process
<1>Step 1:modeling, using CAD / CAE software to simulate and analyze the forging process of high-pressure common rail, according to the simulation results, the structural parameters of the high-pressure common rail die are adjusted and improved until the perfect die structure parameters are obtained;the temperature of the initial simulation parameter in CAD / CAE software is set to 1150 ℃, 1600 tons of hot die forging equipment is selected for simulation, H13 is selected for die material, simple heat transfer is selected between workpiece and die, and friction coefficient between workpiece and die is set as 0.4.
<2>Step 2: manufacturing the die, using the structural parameters of the die obtained in the previous step, manufacturing the pre forging and precision forging die, trimming and cold correction die for the forging of austenitic stainless steel high pressure common rail parts;
<3>Step 3: prepare the raw materials of high pressure common rail, and quickly heat the qualified austenitic stainless steel bar to the preset temperature through medium frequency heating furnace;the austenitic stainless steel bar is directly heated from room temperature to a predetermined temperature, with a heating rate of 55-60 ℃ / s and a predetermined temperature of 1180-1240 ℃.
<4>Step 4 is to prepare the high pressure common rail, and put the raw material heated in the third step into the mold manufactured in the second step to obtain the hot blank of the required high-pressure common rail parts;the closing gap of the mold in manufacturing the high-pressure common rail is 1.7-1.9mm.
<5>Step 5: cooling: the hot high-pressure common rail blank produced in the fourth step is placed in a special air-cooled equipment with controllable temperature and cooling, and the forging forming of high-pressure common rail parts can be completed by moving at a preset speed;
<6>Step 6: finish machining, the cold corrected high-pressure common rail blank is processed by corresponding CNC to obtain austenitic stainless steel high-pressure common rail parts which can work continuously under high-pressure, high-temperature and high-humidity environment.the cooling rate of the high-pressure common rail blank in the air-cooled equipment is 8-13 ℃ / s, the temperature of the high-pressure common rail blank is reduced from 1000-1100 ℃ to 200-220 ℃, and the monitoring inlet temperature of the air-cooled equipment is not lower than 950 ℃.


Hot Tags: stainless steel high voltage parts, China stainless steel high voltage parts manufacturers, suppliers, factory, Copper Die Casting Part, Sand Casting Stainless Steel, Zinc Casting Part, Furniture Zinc Die Casting, Alloy Gravity Casting, Sand Casting Set



Send Inquiry
